You are here: Home » Blog » Strategic Sourcing & Demand Planning: Securing Long-Term Allocations for Pharmaceutical Intermediate CAS 138229-59-1
Strategic Sourcing & Demand Planning: Securing Long-Term Allocations for Pharmaceutical Intermediate CAS 138229-59-1
Views: 0 Author: Site Editor Publish Time: 2026-10-20 Origin: Site
Commercial Context & Therapeutics Demand Growth
In the highly regulated and capital-intensive global pharmaceutical industry, procurement directors and active pharmaceutical ingredient (API) sourcing managers face continuous pressure to secure stable, high-purity precursor pipelines. Methyl 3-formyl-2-nitrobenzoate (CAS No. 138229-59-1) represents an indispensable aromatic building block, serving as a critical upstream precursor in the synthesis of advanced targeted oncology therapeutics—including PARP inhibitors like Niraparib and hypoxia-inducible factor (HIF) stabilizers like Roxadustat.
As global healthcare markets expand access to specialized targeted therapies, demand for reliable, commercial-scale quantities of CAS 138229-59-1 has accelerated. Transitioning from reactive spot-market purchasing to structured, long-term procurement partnerships allows enterprise buyers to insulate their manufacturing schedules against sudden supply crunches and price volatility.
Demand Forecasting & Campaign Synchronization
Managing raw material inventory for multi-step pharmaceutical synthesis requires tight alignment between clinical/commercial sales forecasts and upstream production campaigns:
Strategic Procurement Priorities
Forward Contract Planning:
Structuring multi-quarter supply agreements 3 to 6 months in advance protects procurement budgets from raw material inflation and secures guaranteed volume allocations during peak manufacturing periods.
Production Campaign Alignment:
Coordinating intermediate deliveries with scheduled API batch processing runs reduces onsite inventory carrying costs and prevents warehouse congestion at finishing plants.
Batch Consistency and Yield Predictability:
Securing a guaranteed purity baseline minimizes unexpected lot rejections and costly reactor downtime during downstream processing.
Qualifying a primary manufacturing partner for specialized fine chemical intermediates involves a rigorous evaluation of operational resilience, regulatory compliance, and supply chain transparency:
Sourcing Parameter
Spot-Market Intermediary
Integrated Primary Manufacturer
Strategic Commercial Benefit
Price Stability
Vulnerable to sudden spot spikes
Predictable, direct factory pricing
Lowers direct material COGS
Delivery Reliability
Prone to third-party allocation shifts
Guaranteed volume reservation
Protects master manufacturing schedules
Quality & Traceability
Fragmented documentation
Comprehensive COA & lot tracking
Streamlines inbound regulatory quality audits
Geographic Redundancy
Single-source vulnerability
Dual-site manufacturing footprint
Eliminates regional supply bottlenecks
Global Freight Logistics and Protective Packaging
Safeguarding material integrity across international shipping lanes requires rigorous industrial packaging standards and controlled storage protocols:
Inert Packaging Containment:
Shipped in heavy-duty fiber or steel drums fitted with double-layered polyethylene inner liners to shield the reactive compound from atmospheric moisture, light, and contaminants.
Palletized Export Management:
Standardized loading on heat-treated, shrink-wrapped export pallets designed for seamless ocean containerization and automated warehouse handling.
Warehouse Environment Control:
Storage recommendations mandate dedicated, cool, dry, and well-ventilated chemical facilities maintained below 25 °C, strictly separated from strong oxidizing agents and direct heat sources.
Primary Manufacturing Partner: EASTFINE
For global pharmaceutical brands, contract development and manufacturing organizations (CDMOs), and specialty chemical enterprises, EASTFINE delivers an integrated, reliable primary manufacturing partnership.
Dual-Site Production Security
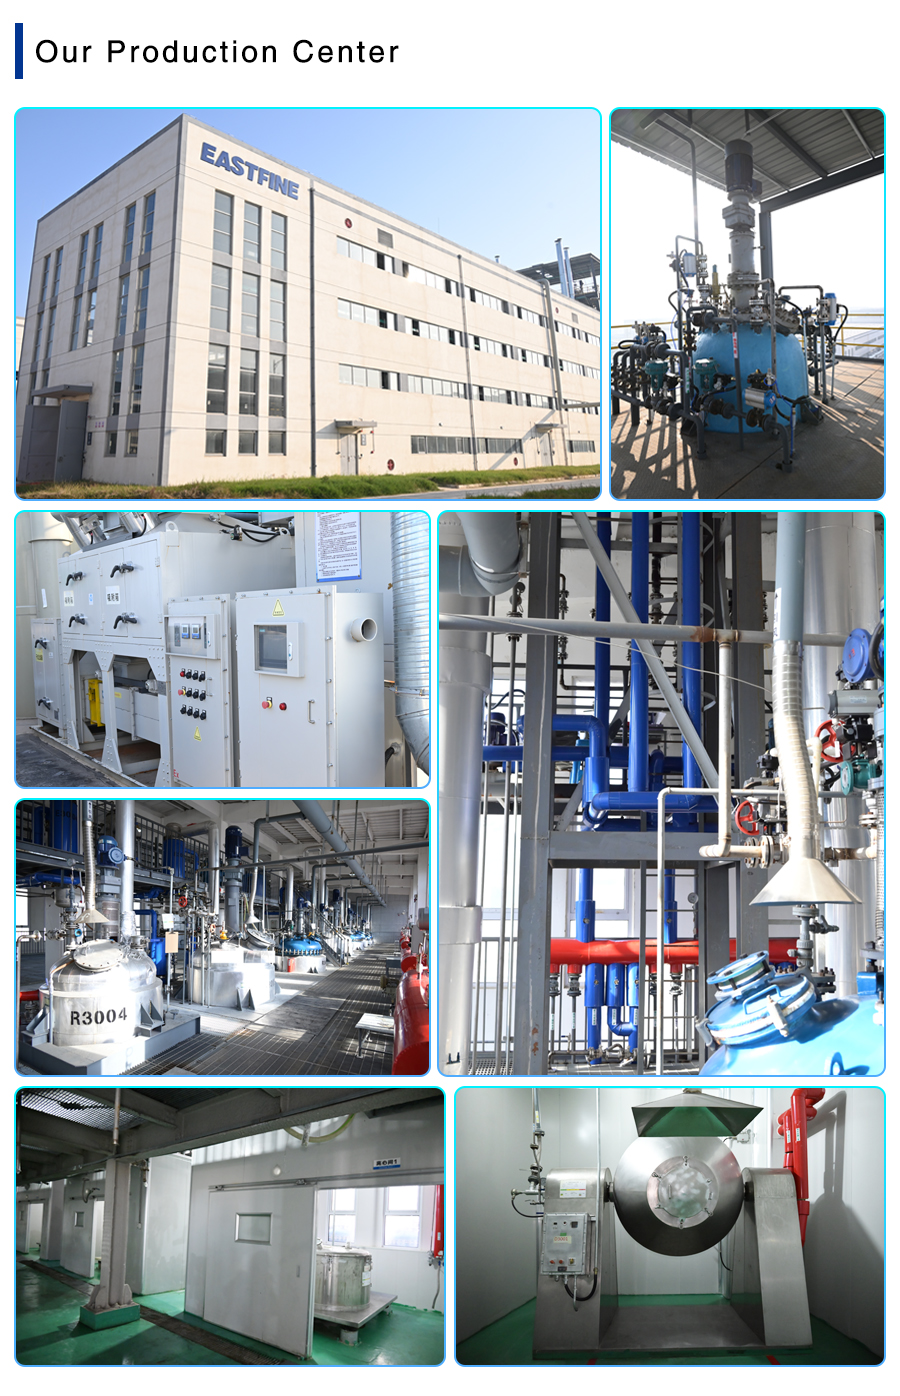
To protect global buyers from supply interruptions, regional environmental maintenance halts, or logistics bottlenecks, EASTFINE operates two fully independent chemical manufacturing complexes in Dalian and Heze:
Uninterrupted Campaign Supply:
Multi-site production capacity guarantees continuous product flow, keeping downstream synthesis schedules running precisely on time.
Scalable Volume Capacity:
Seamlessly scales production from pilot-stage evaluation batches up to multi-ton commercial contract supply.
Patent-Backed In-House R&D & Factory-Direct Value
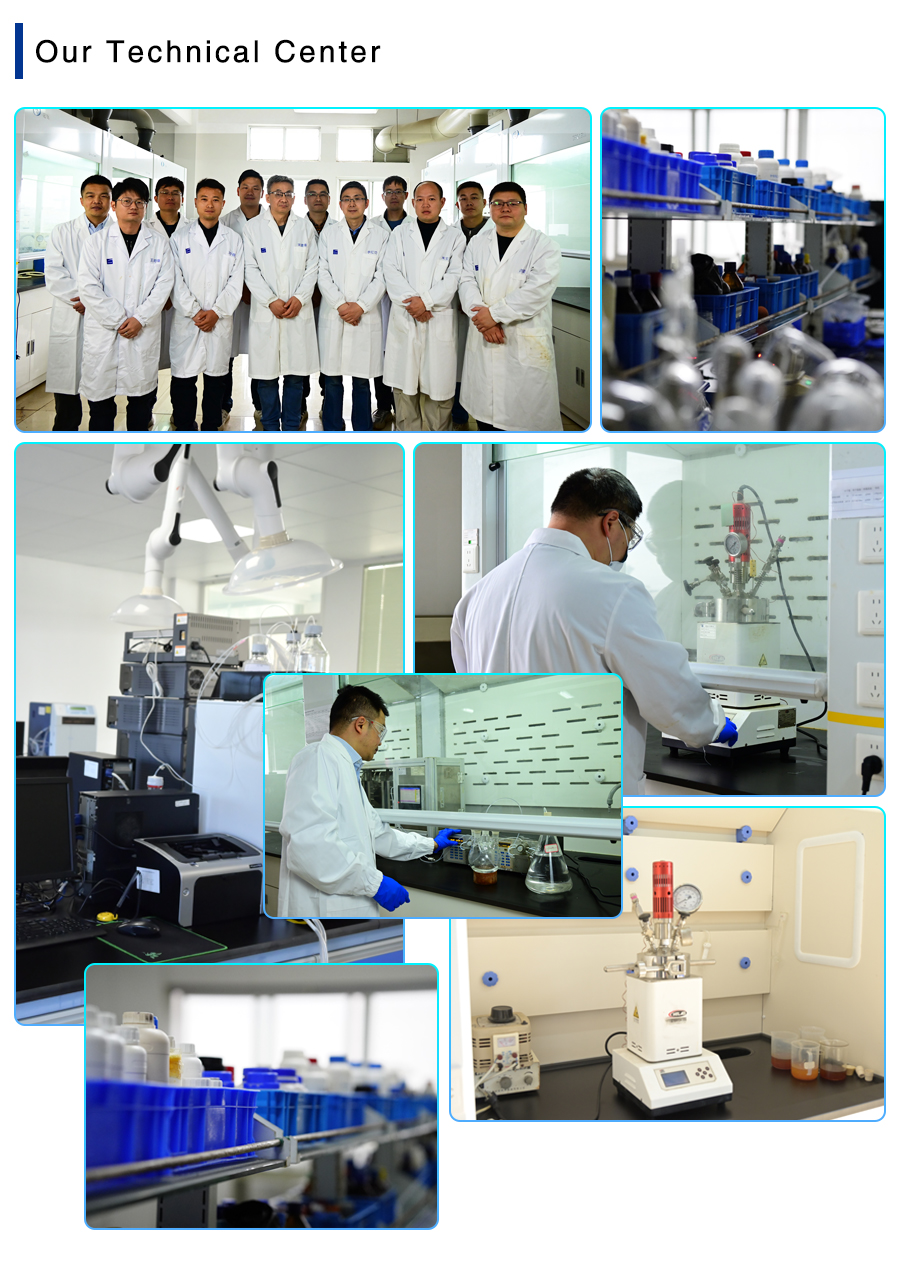
Supported by a dedicated R&D team holding 19 invention patents and 8 utility model patents, EASTFINE continuously optimizes synthesis routes to maximize reaction yields and eliminate unnecessary cost drivers. Sourcing directly from the primary producer eliminates intermediary trading markups, providing transparent, factory-direct terms.
ISO Compliance & Comprehensive Quality Dossiers
Operating under certified ISO 9001, ISO 14001, and ISO 45001 management systems, EASTFINE accompanies every commercial shipment with thorough Certificate of Analysis (COA) testing documentation, sample retention protocols, and complete audit support for global regulatory filings.
Summary & Commercial Inquiries
Methyl 3-formyl-2-nitrobenzoate (CAS No. 138229-59-1) is a vital building block driving efficiency and affordability in modern small-molecule drug manufacturing. Partnering with a primary producer like EASTFINE ensures the supply resilience, cost stability, and quality controls necessary to maintain a strong market position.
To request product samples, Certificates of Analysis, or commercial volume contract pricing, contact EASTFINE's procurement sourcing team today.


 English
 العربية
 Français
 Русский
 Español
 Português
 Deutsch
 italiano
 日本語
 한국어
 Nederlands
 Tiếng Việt
 ไทย
 Polski
 Türkçe
 አማርኛ
 ພາສາລາວ
 Bahasa Melayu
 ဗမာစာ
 Filipino
 Bahasa Indonesia
 magyar
 Română
 Čeština
 қазақ
 Српски
 हिन्दी
 فارسی
 Kiswahili
 Slovenčina
 Slovenščina
 Norsk
 Svenska
 українська
 Ελληνικά
 Suomi
 עברית
 Dansk
 اردو
 Shqip
 বাংলা
 Hrvatski
 Gaeilge
 Eesti keel
 Oʻzbekcha
 latviešu
 Azərbaycan dili
 Български
 ქართული
 íslenska
 Lietuvių


 简体中文